1-805-484-2992
Quotes - Engineering - SalesOverview
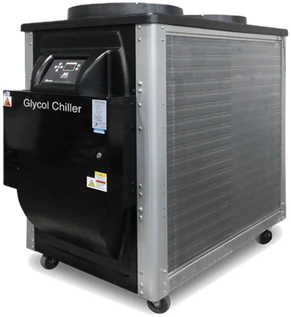
An Advantage glycol package built for a mechanical room, delivering glycol solution at temperatures plain water can't reach.
Advantage indoor glycol units share the same mechanical-room installation as an indoor water chiller, but the evaporator, pump and piping are rated for glycol service and sized to hold the required freeze-protected temperature. They're the right call whenever the process fluid temperature itself needs to run below 32°F, whether or not the unit is ever exposed to freezing weather.
Single-zone models deliver one fluid temperature to the whole loop; dual-zone models produce two independent temperatures from one chiller frame, which is common in food and beverage plants running both a colder product-cooling loop and a milder jacket or CIP-return loop from the same room.
See the BG series for the full part-number line-up of Advantage indoor glycol models on this page, plus every outdoor model; a brewery running multiple tanks off one chiller may also want the BC-SCC tank control cabinet to give each tank its own independent setpoint from that one loop.
- 1.5 to 30 HP, single or dual zone
- Rated for glycol service throughout - evaporator, pump and piping
- Common in breweries, dairies and other sub-freezing process loops
Indoor Glycol Configurations
Zone count and glycol type are chosen together, from the loop the process actually runs.
| Configuration | Range | Notes |
| Single Zone | 1.5 to 30 HP | One glycol temperature plant-wide |
| Dual Zone | 1.5 to 30 HP | Two independent glycol temperatures from one frame |
| Glycol Type | Propylene (food-grade) or ethylene | Propylene standard for food/beverage contact risk |
Sizing the Glycol Mix
The glycol percentage in the loop is set by the coldest leaving fluid temperature the system needs to reach, not by a round-number habit - a 25°F brewery glycol loop needs a meaningfully higher glycol concentration than a 40°F dairy loop, and running more glycol than the application requires just adds pumping cost and reduces heat-transfer efficiency for no benefit. Food-grade propylene glycol is the default in any application with a food or beverage contact risk; industrial ethylene glycol is reserved for closed loops with no such risk, at a lower cost per gallon.
Reservoir sizing on an Advantage indoor glycol unit also has to account for the glycol solution's lower specific heat relative to plain water - the reservoir and pump are sized to the specified mix, which is another reason to confirm glycol type and percentage before, not after, the unit ships.
Glycol Loop Details
What We Need to Size an Indoor Glycol Unit
An indoor glycol unit is sized to the fluid in the loop, so tell us about the mix as well as the temperature you need:
- Coldest supply temperature, and whether a second zone runs warmer
- Food-grade propylene or industrial ethylene glycol
- Mix percentage, or the freeze point it has to protect to
- How many tanks, jackets or loops the unit will feed
- Process pump horsepower, since its heat stays in the loop
- Mechanical room space, ventilation and electrical service
Call and talk it through with an engineer: 1-805-484-2992