1-805-484-2992
Quotes - Engineering - SalesOverview
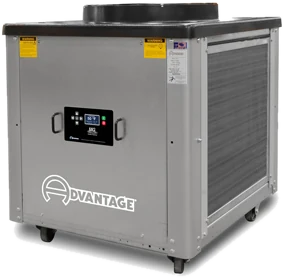
The workhorse Advantage MG range for single-machine plastics, machine-tool coolant and mid-size process cooling.
This is the size range most single injection-molding presses, CNC machine tools and mid-size lasers actually need. Advantage MG units are available air-cooled for the simplest installation, or water-cooled where the mechanical room runs hot or floor space matters more than a condenser fan's footprint.
Remote-condenser (ARC) variants are available through this range: the compressor and pump stay at floor level next to the machine, and the condenser coil mounts outdoors or on a roof, connected by refrigerant lines. That keeps the noisy, heat-rejecting half of the chiller out of the production floor without moving to a full central system.
As with the smaller frames, tell us the actual heat load and required fluid temperature rather than working backward from a competitor's nameplate tonnage - a molding press's heat load depends on shot size, cycle time and material as much as clamp tonnage, and sizing from clamp tonnage alone is a common and expensive mistake. Every MG model in this tonnage range has its own part-number page with full specs; browse individual MG models to match the right one to your load.
- Air-cooled, water-cooled, and remote-condenser (ARC) configurations
- Factory-piped pump and reservoir - drop in place and connect
- Suitable for single-press plastics, CNC coolant loops, mid-size lasers
- EDM machine-cooling variants available in this range as well
Three Ways to Reject the Heat
Same MG chiller, three condenser arrangements - pick by where the heat can go.
| Configuration | Capacity Range | Notes |
| Air-Cooled | 2 to 15 tons | Simplest install, no plant water connection |
| Water-Cooled | 2 to 15 tons | Smaller footprint, needs plant/tower water supply |
| Remote Condenser (ARC) | 2 to 15 tons | Compressor/pump indoors, condenser coil outdoors or on roof |
Sizing From Heat Load, Not Clamp Tonnage
A common and expensive mistake in this range is sizing a chiller off the molding press's clamp-force tonnage rather than its actual process heat load. Clamp tonnage measures the press's clamping force; chiller tonnage needs to match the BTU/hr the mold and material actually generate, which depends on shot size, cycle time, material type and mold design. Two presses with the same clamp tonnage can need very different chiller sizes.
Every Advantage unit in this range ships factory-piped and pressure-tested - the reservoir and pump are already sized and plumbed to the compressor, so installation is a matter of setting the unit, connecting power, and running supply/return lines to the point of use.
Machine-Side Data
What We Need to Size Your MG Portable
MG units in this range are sized from actual heat load, not clamp tonnage, so the most useful thing you can send is the machine's real load:
- Heat in BTU/hr or tons, or resin pounds per hour for a molding press
- For a laser, the cooling requirement from its installation sheet
- Fluid temperature the mold, tool coolant or laser needs, and the air temperature at the unit
- Air-cooled, water-cooled, or an ARC condenser mounted outdoors
- Voltage, phase and floor space beside the machine
Call and talk it through with an engineer: 1-805-484-2992